
Dairy Homogenizer Machine Price: Buyer and Selection Guide
When a procurement lead in Monterrey accepted a low initial quote for a new dairy line, the choice looked efficient. It changed once the review added cleaning provisions, validation evidence, and expected downtime. Nothing had broken; the budget simply no longer covered the process. The team recovered by rewriting its request around product viscosity, target particle reduction, sanitation, throughput, and service access. The issue was not the machine alone, but judging purchase price before defining the application and total cost.
Summary: A useful dairy homogenizer machine price comparison starts with duty, hygienic design, verification, and lifecycle support—not the number on a quotation. Convert pressure consistently: 1 MPa equals 10 bar. Then compare delivered flow at the required pressure and product condition. For food operations, the FDA Food Safety Modernization Act frames preventive controls around the facility and process, rather than a machine label. Before comparing commercial terms, ask suppliers for a documented application basis, cleaning approach, and acceptance plan.
The milk homogenizer machine market spans very different duties: pilot development, short production runs, continuous dairy processing, and high-shear dispersions that happen to be food products. A dairy homogenizer for sale is not a like-for-like option until the buyer defines the feed, target result, operating window, and ownership responsibilities. Search terms may surface suppliers, but they cannot replace an application brief.
Start with the dairy duty, not the quoted machine
Homogenization may be selected to reduce fat globule size distribution, improve dispersion stability, or deliver repeatable texture. In milk, cream, cultured products, ice-cream mix, and protein-rich formulations, identical pressure settings can give different results. Composition, inlet temperature, fat level, solids, and viscosity all affect the response. A data sheet alone does not prove that a unit will meet a product target.
Specify the process window
Set the nominal flow and the minimum and maximum flow the line must sustain. State pressure in one unit, such as MPa or bar, and record the maximum allowable product-temperature rise. A 20 MPa requirement is 200 bar; this simple conversion prevents mixed-unit comparisons. Also specify whether one or two homogenization stages are required, along with inlet condition, particle or stability target, and the sample plan used to prove the result.
Map the homogenizer to upstream separation, blending, and pasteurization, as well as downstream filling or fermentation. Capacity depends on both the formulation and the usable operating point. Illustrative only: a line specified at 5,000 L/h is not comparable if it can deliver that flow only below the required pressure or with a low-viscosity test liquid. Require each quote to state flow and pressure at the same duty point.
Food safety controls apply to the full operation. FDA FSMA materials describe preventive controls for covered food facilities, while the FAO food safety program provides broader context. Neither source certifies a homogenizer; together, they help frame hygienic construction, sanitation, traceability, and records.
Compare lifecycle cost drivers before comparing total price
There is no defensible universal price. Configuration, capacity, pressure, materials, controls, documentation, installation scope, and local support can all change a commercial proposal. A low purchase figure may suit a simple, well-understood duty. It becomes risky when it excludes the components or evidence needed to operate, clean, validate, and maintain the line.
| Comparison point | What to request | Why it affects value |
|---|---|---|
| Delivered duty | Flow and pressure at the actual product condition | Separates a stated maximum from usable production capacity. |
| Hygienic integration | Product-contact materials, seals, connections, and cleaning route | Influences sanitation consistency and changeover planning. |
| Controls and records | Instrumentation list, alarms, data needs, and acceptance documentation | Supports repeatability and investigation when a batch varies. |
| Serviceability | Wear-part plan, access steps, lead times, and training scope | Shapes planned maintenance and unplanned downtime exposure. |
| Scale-up path | Pilot conditions and production correlation plan | Reduces the risk of buying a production unit from an unrepresentative trial. |
Build a total-cost worksheet from one-time and recurring assumptions, and keep exclusions visible. If a supplier offers testing or commissioning, identify the evidence included. An illustrative lifecycle review can model energy, cleaning chemicals, wear parts, service labor, lost output, and qualification effort. It cannot treat assumed savings as a guarantee.
| Cost driver | Questions for the quotation | Lifecycle implication |
|---|---|---|
| Capacity and pressure duty | What operating point is warranted for this formulation? | Higher duty can change component selection, utility load, and maintenance planning. |
| Product-contact design | Which materials, elastomers, and surface requirements are supplied? | Compatibility affects cleanability, replacement choices, and product risk. |
| Cleaning and sanitation | What CIP connection, sequence assumptions, and validation support apply? | Cleaning time and verification effort affect availability and release confidence. |
| Controls and automation | Which sensors, interlocks, recipes, and records are included? | Integration scope may alter project engineering and operator workload. |
| Commissioning and support | Who installs, trains, services, and supplies critical parts? | Response time and documentation can materially affect recovery from downtime. |
Choose the equipment class that matches the process
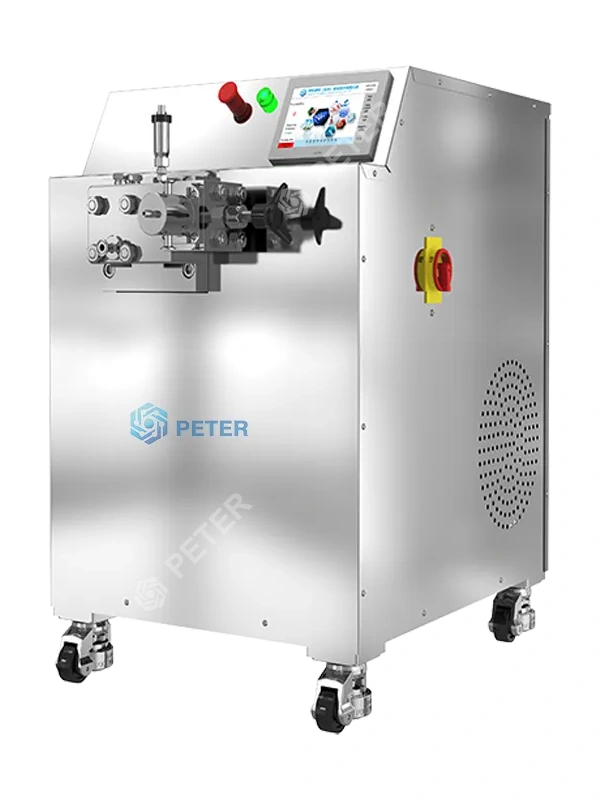
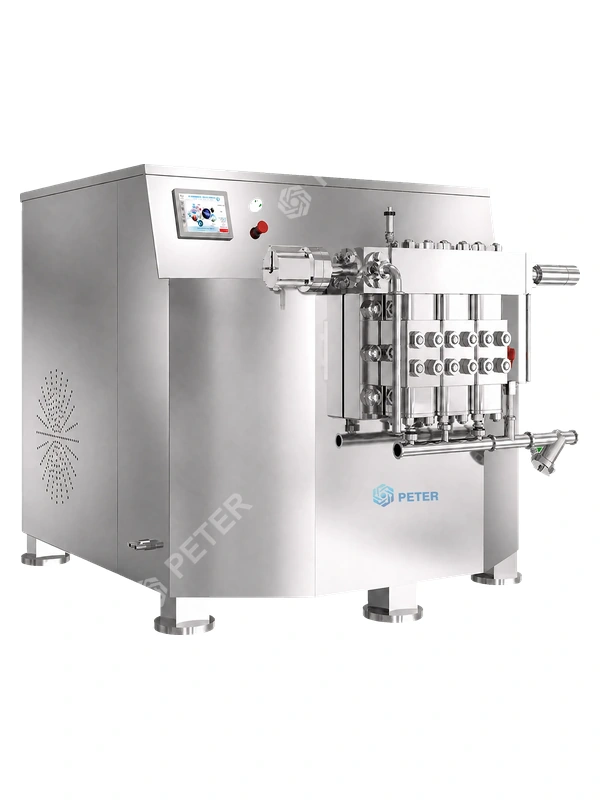
Conventional high-pressure homogenizers use pumping and a homogenizing valve or interaction zone to apply controlled mechanical forces. Microfluidizer-style systems may suit controlled flow paths, development work, or particular dispersion targets. High-shear mixers, colloid mills, and inline emulsifiers can support blending or pre-dispersion, but they are not interchangeable with a high-pressure system without product trials.
For scale-up, record more than the formulation: test equipment, flow, pressure, number of passes, inlet temperature, hold conditions, sample point, and analytical result. Where its scope applies, ISO 72458 is a test method, not a product certification; it does not establish that every dairy process is compliant. The buyer should identify the method for particle sizing, stability, viscosity, microbiological controls, or other critical quality attributes, then agree acceptance limits with the producer.
New equipment generally provides a current specification, configurable controls, and a documented commissioning path. Used equipment may suit a constrained budget when the duty is known, but assess its history, product-contact condition, parts availability, cleaning suitability, safety systems, and documentation before assigning value. On a food line, a physical inspection and written gap list are usually more useful than a broad claim that equipment is “refurbished.”
Define compliance, validation, and supplier responsibilities
A purchase order does not transfer compliance. The destination market, product category, intended use, facility controls, and marketing claims determine which requirements apply. FDA FSMA materials concern food-safety preventive controls, while FAO resources provide international food-safety context. They are not machine certificates. Claims that a machine alone makes a process compliant can create procurement, customer-audit, and claim-management risk.
For explicitly qualified pharmaceutical comparisons, FDA cGMP regulations can guide discussion of documentation and quality systems. They do not automatically apply to dairy equipment or imply pharmaceutical compliance for food. Ask the supplier which documents it can provide: drawings, material information, operating manuals, test records, spare-parts recommendations, and agreed acceptance evidence.
Turn the specification into a selection decision
- Write a one-page application brief covering formulation, throughput range, pressure range, inlet condition, target quality attributes, cleaning route, utilities, and installation constraints.
- Request a comparable duty-point statement from each supplier, including what liquid or product was used for any performance test.
- Set acceptance criteria before purchase: sample locations, test methods, limits, documents, and the responsible party for corrective action.
- Evaluate service access by location, including recommended spares, training, remote support, and realistic lead-time assumptions.
- Score total cost with the same assumptions for every bid, while keeping purchase cost, integration, operation, maintenance, and risk visible as separate lines.
For buyers sourcing from China, CAS PETER may be included in a structured RFQ process when configurable high-pressure equipment, application discussion, and documentation are in scope. Compare a dairy homogenizer machine for production duty and a dairy homogenizer for sale for a smaller application against the same written duty point, not headline capacity alone. Background guidance is available on choosing a pressure homogenizer and how high-pressure homogenizers work.
Frequently asked questions
How much does a milk homogenizer cost?
Cost depends on the required duty and commercial scope, so a generic figure is not a reliable basis for buying. Compare quotations only after they specify flow, pressure, hygienic design, controls, documentation, testing, and service assumptions. Request an itemized proposal and identify exclusions before setting the budget.
What affects the price of a milk homogenizer?
Capacity, pressure, formulation characteristics, product-contact materials, cleaning design, automation, validation support, installation scope, and service coverage all affect price. A high specification is not always necessary, but each omitted requirement should be an intentional process decision. Link every option to a stated risk, quality target, or operating need.
How do new and used milk homogenizers compare?
New equipment can be specified for the intended process and supplied with an agreed testing and documentation plan. Used equipment can be viable when inspection confirms its condition and the gaps in cleaning, safety, parts, and process fit are acceptable. Compare the cost to restore, verify, and support the unit—not just its asking price.
How should buyers assess dairy homogenizer for sale before choosing a milk homogenizer?
Start with the application brief and require each supplier to respond to the same flow, pressure, product, cleaning, and acceptance criteria. Review evidence for the quoted operating point, available documentation, and the support route in the destination market. A trial or agreed test protocol is particularly valuable when formulation behavior is not established.
References and next step
- U.S. Food and Drug Administration, Food Safety Modernization Act
- Food and Agriculture Organization of the United Nations, Food Safety
- International Organization for Standardization, ISO 72458 – test method scope should be checked for the intended use.
- U.S. Food and Drug Administration, Current Good Manufacturing Practice regulations – relevant only for explicitly qualified comparisons.
A dairy homogenizer earns its place through a repeatable process, not a low number on page one of a quote. When the decision reaches the RFQ stage, contact CAS PETER with the application brief to discuss a configured high-pressure homogenizer and the evidence needed for selection.