
Yeast Cell Disruption: High-Pressure Homogenization Trial Guide
Yeast cell disruption by high-pressure homogenization should be optimized against recovered product quality, not the largest pressure setting or the highest count of broken cells. Begin with a representative yeast suspension, an approved equipment operating window, controlled cooling and a defined assay for the desired fraction. Sample after separate passes and compare cell opening, target recovery, activity and clarification behavior. Stop when additional processing no longer improves the accepted product. There is no universal pressure-and-pass recipe that transfers reliably between yeast strains, growth conditions, targets or homogenizer designs.
This guide focuses on planning a yeast-specific development trial. For the broader equipment and mechanism overview, see our high-pressure cell-lysis guide. The trial framework below helps connect the disruption step to the extract or cell-wall fraction your downstream process actually needs.
Start with the yeast fraction you want to recover
A soluble intracellular enzyme, a structural cell-wall ingredient and an insoluble recombinant product require different acceptance tests. A treatment that releases more total soluble material may also increase impurities. A treatment that breaks walls extensively may make the desired wall fraction harder to separate. Write down the destination of the target before deciding how aggressively to process the biomass.
For a soluble enzyme, the primary result might be total recovered activity after a fixed clarification procedure. For a protein ingredient, it might be accepted protein mass with a defined composition. For a wall fraction, include the composition and recoverability of the solid material. These are proposed development endpoints, not interchangeable definitions of disruption efficiency.
Published work on biopolymer release from Saccharomyces cerevisiae biomass investigated cell-wall constituents as the desired products. Its application differs from recovering an active intracellular enzyme. That difference is a useful reminder to match the experiment to the intended fraction rather than borrowing an attractive result from a different application.
Why a bacterial or mammalian-cell recipe is a poor starting specification
Yeast has a cell wall as well as a membrane. Strain, physiological condition, cultivation and harvest history can affect how a suspension responds. Record the species and strain, culture stage, washing procedure, storage time and any freeze–thaw history. A result obtained from freshly harvested laboratory biomass should not silently become a specification for stored industrial biomass.
Keep concentration definitions explicit. Grams of dry biomass per litre, wet-paste mass fraction and optical density describe different things. If the production team uses wet paste, document its preparation and water content assessment rather than treating it as an exact substitute for dry-cell concentration. Consistent feed preparation makes later comparisons more interpretable.
Our mammalian-cell homogenization article addresses a different starting material. Likewise, the site’s E. coli process reference does not establish yeast pressure settings, yield or activity retention.
Define a trial matrix that can explain the result
First agree the permitted pressure range, feed suitability, temperature limits and operating procedure with the equipment supplier and the responsible process team. The machine’s maximum rating is a boundary, not a recommended yeast treatment. Do not modify pressure-containing components or bypass protective controls to extend a trial.
Within the approved window, compare a small number of justified pressure conditions and collect samples after defined separate passes. Hold feed preparation, starting concentration and analytical methods consistent. If you change pressure, concentration and cooling simultaneously, a better result will not tell you which change mattered. Use independent repeat trials where the decision requires evidence of reproducibility.
| Trial question | What to record | Decision it supports |
|---|---|---|
| Are more cells opening? | Consistent microscopy or another qualified disruption assessment | Whether mechanical treatment is changing the biomass |
| Is the desired fraction increasing? | Target mass or total activity after identical sample handling | Whether further disruption creates useful recovery |
| Is quality deteriorating? | Activity, identity or other target-specific quality attributes | Whether additional exposure is becoming harmful |
| Can the lysate be clarified? | Recovered volume, separation time and target distribution between fractions | Whether the apparent gain survives downstream processing |
| Will the recipe transfer? | Machine configuration, actual flow, pressure history and temperature history | What a pilot confirmation run must reproduce or reassess |
This is a proposed decision table for development work. It supplies no universal pressure, lysis percentage or equipment performance guarantee.
Measure opening, extraction and activity separately
A cell-opening assessment answers a structural question. A protein assay answers a composition question. An enzyme assay answers a functional question. One result cannot substitute for the others. Include an untreated control and specify how samples are diluted, held and clarified before analysis. Check that the assay works in the actual buffer and lysate matrix.
A study of protease extraction from brewer’s spent yeast reported disruption, protein extraction and proteolytic activity separately. Greater visible disruption did not provide a simple rule for the best activity result. The study also cautioned that its glass-bead procedure was not a validated comparison with a commercial bead mill. These findings support careful endpoint selection; they are not CAS PETER test results.
Track the target through both supernatant and solids when its distribution matters. A decrease in the clarified liquid does not necessarily mean destruction: adsorption, precipitation or a changed separation outcome may also matter. Use the measurements needed to distinguish those possibilities before adjusting the machine recipe.
Use a recovery calculation with an honest denominator
For an activity-based comparison, total recovered activity equals measured activity concentration multiplied by recovered volume, with dilution corrections applied once. For example, a hypothetical clarified extract of 0.80 L at 1,200 units/L contains 960 units. Another condition producing 0.60 L at 1,500 units/L contains 900 units. The more concentrated sample yields less total recovered activity in this example.
Those numbers are illustrative arithmetic, not experimental data. They show why concentration alone can mislead. If you normalize activity to dry biomass, use the same dry-biomass basis for every condition. Report total recovered units and units per gram of input dry biomass alongside the accepted quality result.
Do not call a result “90% recovery” unless the denominator is defined and measured or otherwise justified. Recovery relative to a qualified exhaustive extraction reference differs from recovery relative to an earlier process. When the total recoverable target is unknown, report measured units per gram and the comparison basis rather than inventing an absolute percentage.
Control the whole temperature and holding history
Record feed temperature, temperature near the discharge at a defined location and temperature after any cooler. A cold collection bottle does not prove that the material avoided a short hot exposure upstream. Use an appropriate measurement arrangement confirmed for the equipment and process; an improvised probe must not compromise the pressure boundary or containment.
Keep the time between treatment and assay consistent. If later samples wait longer for clarification, the comparison may include storage effects as well as homogenization effects. Define collection order, cooling, hold duration and the allowed interval before analysis. The separate guide to homogenizer temperature rise explains the thermal question in more detail.
Stop criteria should include the product’s agreed temperature and quality limits, abnormal equipment behavior and loss of controlled feed conditions. For pressure-system hazards, follow the manufacturer’s instructions and the applicable local requirements. The HSE pressure-systems guidance provides general safety context; it is not a yeast-processing protocol.
Distinguish complete separate passes from tank recirculation
A complete separate pass transfers the defined batch through the processor into a separate receiving vessel. Tank recirculation mixes material with different treatment histories. Flow multiplied by elapsed time and divided by tank volume gives nominal turnovers; it does not prove that every portion received an equal number of passes.
For a screening study, a clearly documented separate-pass arrangement can make sampling easier to interpret. If production will use recirculation, validate that arrangement later rather than assuming the laboratory result transfers unchanged. Include tank mixing, collection losses and the sampling location in the record. Our comparison of process flow arrangements covers this distinction.
Compare bead milling only when it answers a real process decision
Bead-based disruption may be worth evaluating when sample format, batch size or the desired wall fraction makes it relevant. Compare methods using representative feed and the same final acceptance criteria. Equal processing minutes or equal motor power does not establish equal treatment. Include bead separation, sample recovery, cooling and cleaning in the comparison boundary.
For background on that alternative, see the bead-mill process guide. Do not select a method solely because one produces a visually clearer or more disrupted sample. The useful comparison is accepted target recovered through the intended downstream workflow.
Turn laboratory evidence into a useful equipment enquiry
Provide the supplier with the yeast identity, biomass preparation, concentration basis, batch volume, target fraction and current analytical method. Add acceptable temperature exposure, required containment, cleaning expectations and the intended process arrangement. Ask which feed and operating limits apply to the proposed configuration.
The CAS PETER PT-20 laboratory homogenizer is a product page for an equipment discussion, not proof of performance on your yeast. Request a representative-material trial and a report showing recovered target, actual flow, thermal history and product losses. For scale-up, reassess flow-path differences, cooling and downstream separation instead of copying pressure alone.
Watch the physical process
GreenCoLab’s educational demonstration shows high-pressure homogenization for cell disruption using an algal material. It illustrates the process concept; it does not supply a yeast recipe or validate the equipment discussed here.
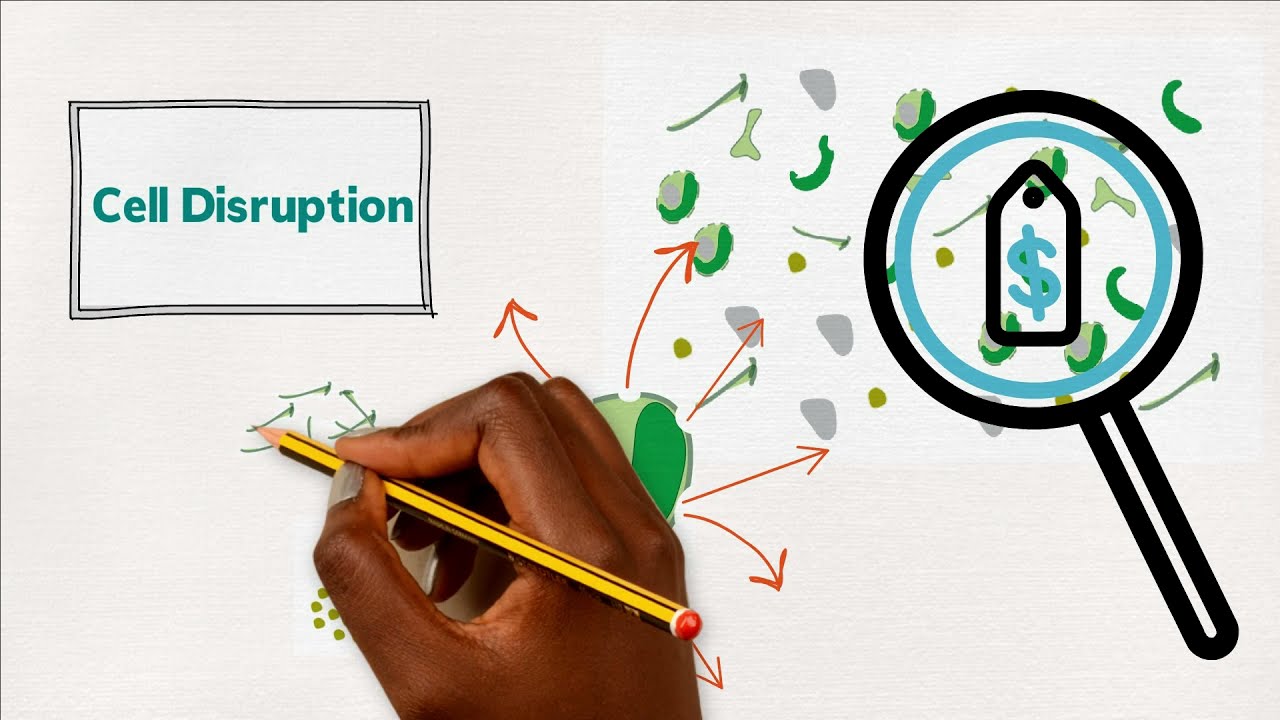
Watch the GreenCoLab demonstration on YouTube.
Frequently asked questions
What pressure should be used for yeast cell disruption?
Establish pressure through a representative trial inside the approved equipment and product limits. Yeast identity, concentration, target fraction, flow path and temperature history prevent a universal setting from being reliable.
Does a higher cell-disruption percentage mean a better extract?
Not necessarily. Measure the desired target after the same clarification procedure and assess its quality or activity. More opening can also change impurities and separation behavior.
How many homogenizer passes does yeast need?
Use pass-by-pass evidence to identify when further processing stops improving accepted recovery. Define whether the experiment uses separate complete passes or tank recirculation before comparing results.
Can E. coli settings be reused for yeast?
They should not be treated as a qualified yeast recipe. Use them only as background information and develop a yeast-specific operating window with suitable acceptance tests.